Continuous Casting Equipment
High-precision pinch panels for continuous casting plants — manufactured to client billet cross-section and casting speed requirements. DNL manufactures the water-cooled pinch panel.
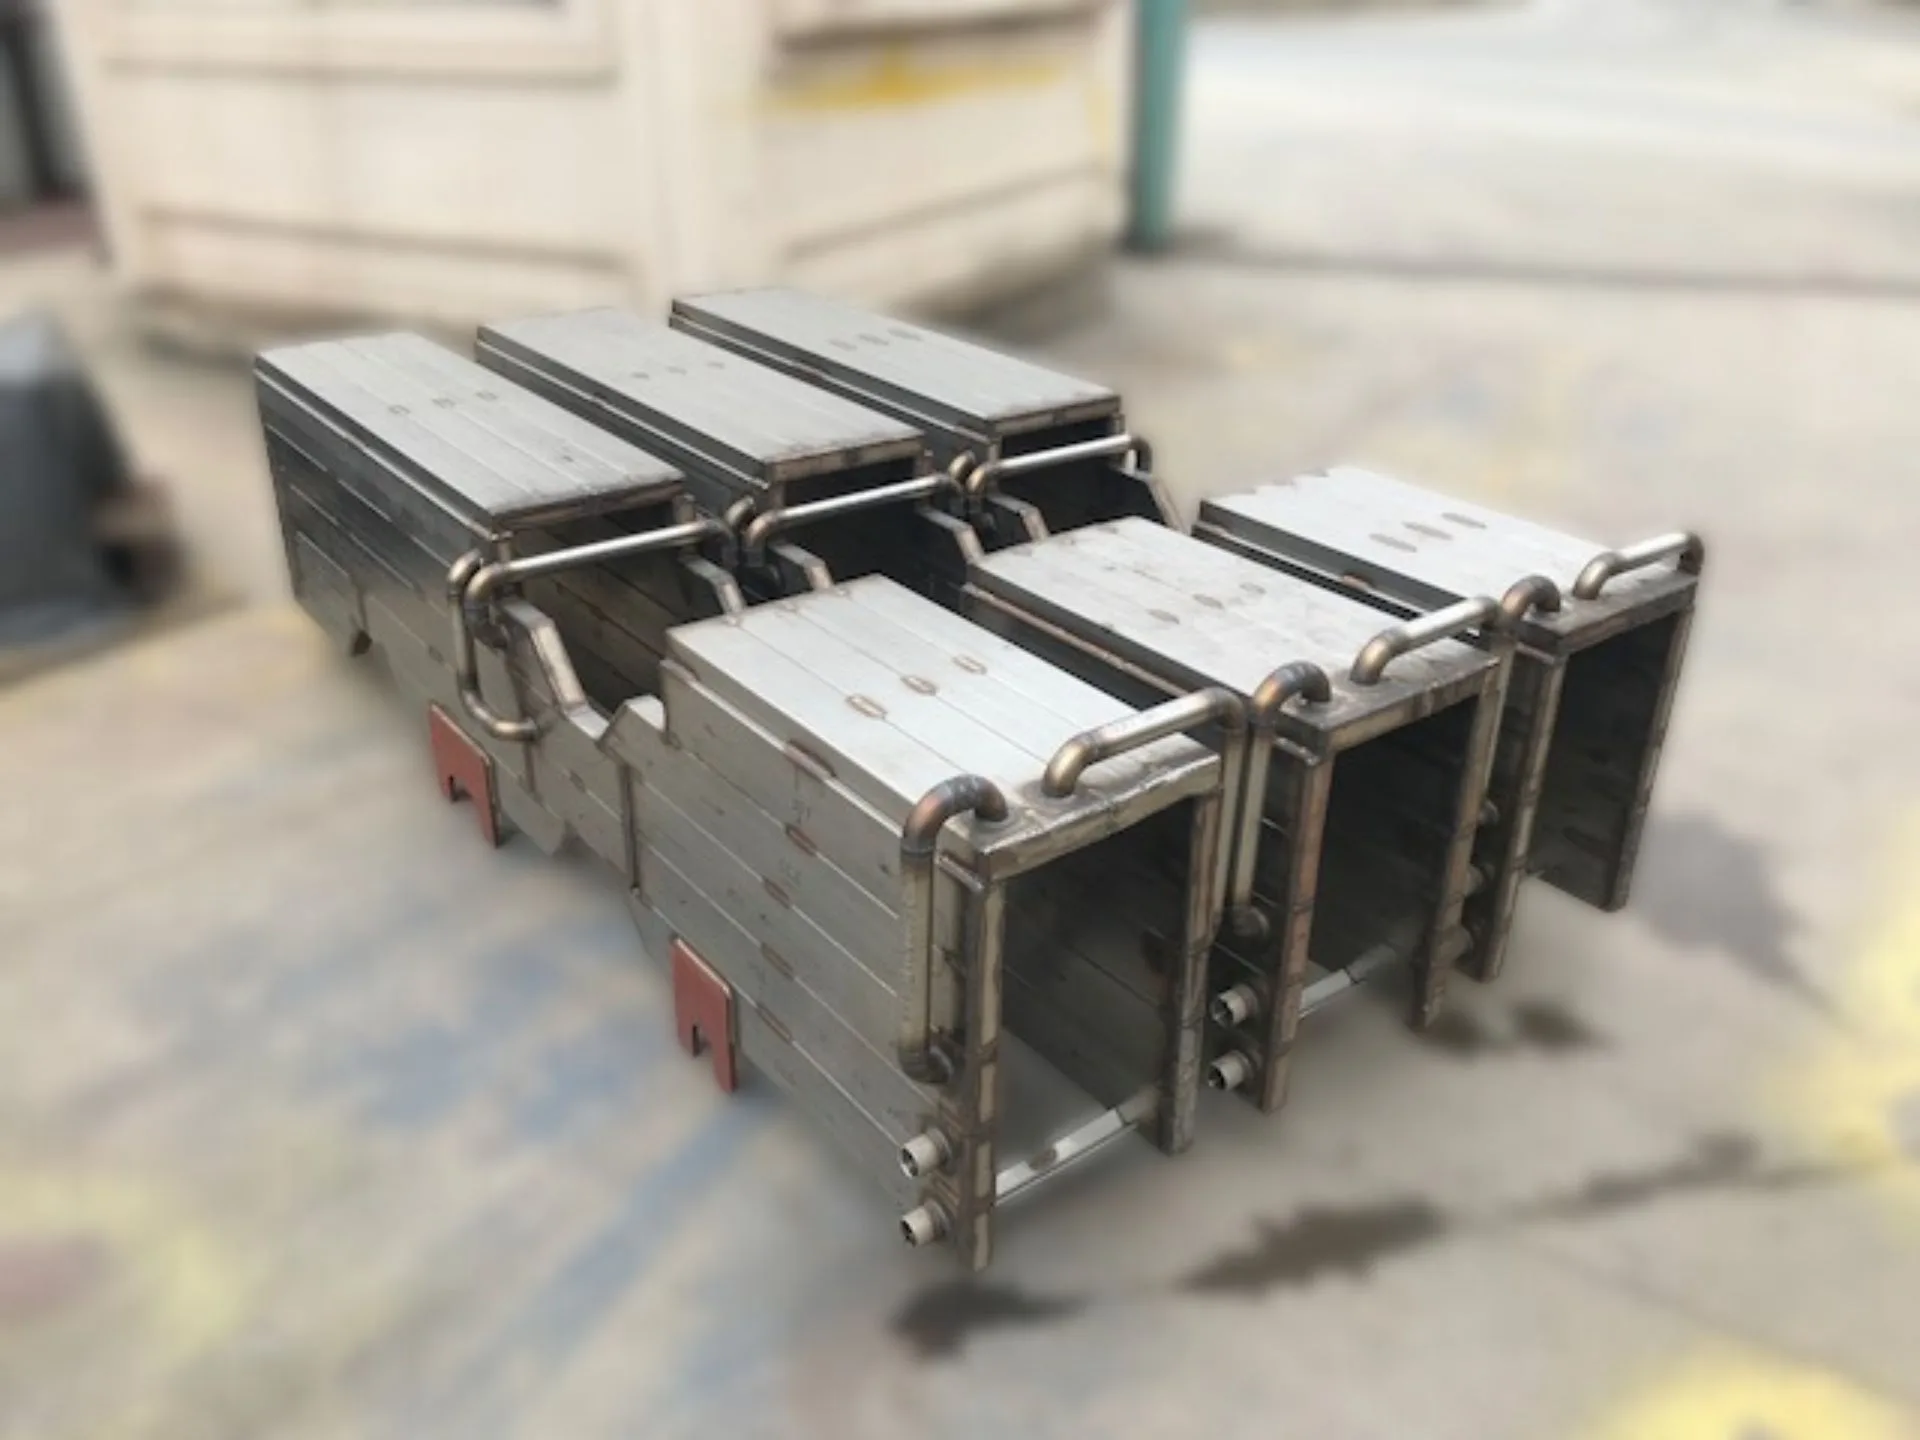
| Custom manufacturing to client billet cross-section |
| High-precision mechanical design |
| Warranty period: 12 months |
It protects the withdrawal-straightening machine from the billet's radiant heat. The billet still arrives at this zone glowing hot: US patent 7,909,086 gives a billet surface temperature of 900–1200 °C at the entry to the final solidification cooling zone, and the withdrawal-straightening unit sits right after this zone. The panel shields the roll stand and bearings from that radiant load.
Because solidification is not yet complete. Publications from the University of Illinois Continuous Casting Consortium show that a liquid core remains inside the shell as it leaves the mould; the depth of this core ranges from 5 to 30 meters depending on casting speed and section thickness, and solidification continues through the spray chamber. The withdrawal-straightening zone sits at the end of this process.
Because it becomes unsuitable for straightening as it cools. US patent 4,106,547 states that once the billet cools enough, its bending resistance rises above what the straightening machine can overcome. The billet must be straightened while still hot, which commits the machine to a high radiant load and makes the water-cooled protective panel necessary.
DNL Mühendislik manufactures the water-cooled pinch panel. The panel is produced to the client's billet cross-section and casting speed.
