Continuous Casting Equipment
DNL manufactures components for continuous casting billet casters, made to the customer's capacity and billet size — reliable and efficient process solutions.
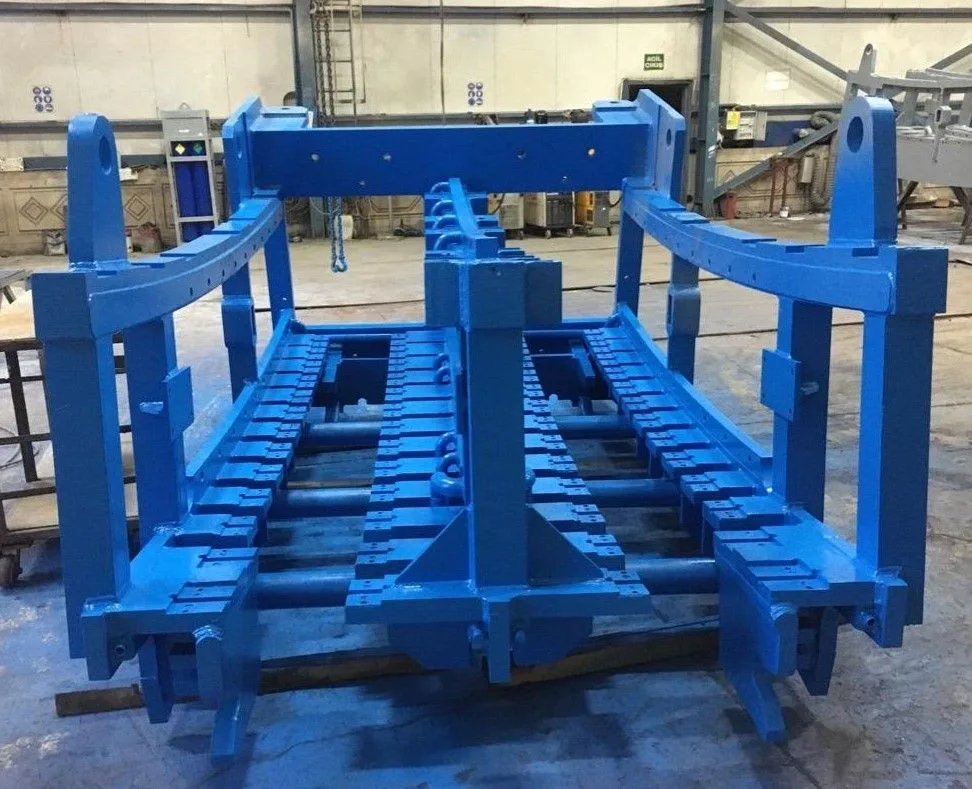
| Custom design to client capacity and billet size |
| Industrial-standard mechanical components |
Far higher than an arc furnace panel. A numerical study on a high-speed billet mould gives an average heat flux of about 2.4 MW/m² between the billet shell and the mould at a casting speed of 4–4.5 m/min. For comparison, an arc furnace wall panel's peak value is on the order of 600–700 kW/m² (Toulouevski & Zinurov, Innovation in Electric Arc Furnaces, 2nd ed., Section 12.3.1).
As the solidifying shell cools it shrinks and starts pulling away from the mould wall; an air gap forms and heat transfer degrades. The taper compensates for this shrinkage and maintains contact. The University of Illinois's continuous casting heat transfer model calculates the ideal taper from shell shrinkage. Because operating speed in high-speed billet casting can reach 4–4.5 m/min, the taper is especially decisive.
Copper moulds, water-cooled pinch panels and machine components. DNL Mühendislik manufactures these parts to the customer's billet cross-section and casting speed.
